| Portable, split-frame machine | On-site maintenance, repair, and work on installed pipe where moving the workpiece is impractical. | Depending on the tooling, can perform external or internal chamfering, beveling, and end facing. | Check the machine’s stated pipe outside-diameter range, available clamping inserts, wall-thickness limits, and clearance around the pipe. | Can be fitted around fixed pipe; avoids transporting large or installed workpieces to a stationary shop machine. | Setup and alignment are important; access, clamping conditions, and the operator’s skill can affect results. | Request a demonstration on the actual pipe material and dimensions. Verify power requirements, tool availability, and whether the quoted tooling covers the required operation. |
| Stationary, single-station chamfering machine | Workshops producing repeat chamfers on a defined range of pipe or tube sizes. | Primarily repeatable edge chamfering or deburring; some configurations also provide facing or other end-preparation operations. | Capacity depends on the chuck, tooling, machine layout, and pipe geometry. Confirm both the minimum and maximum workpiece sizes. | Dedicated setup can make routine jobs straightforward and repeatable when parts and requirements are consistent. | Less adaptable if jobs vary widely; changing sizes or operations may require tool changes and setup time. | Check clamping method, adjustment range, cycle controls, tool-change procedure, guarding, and sample-part finish. |
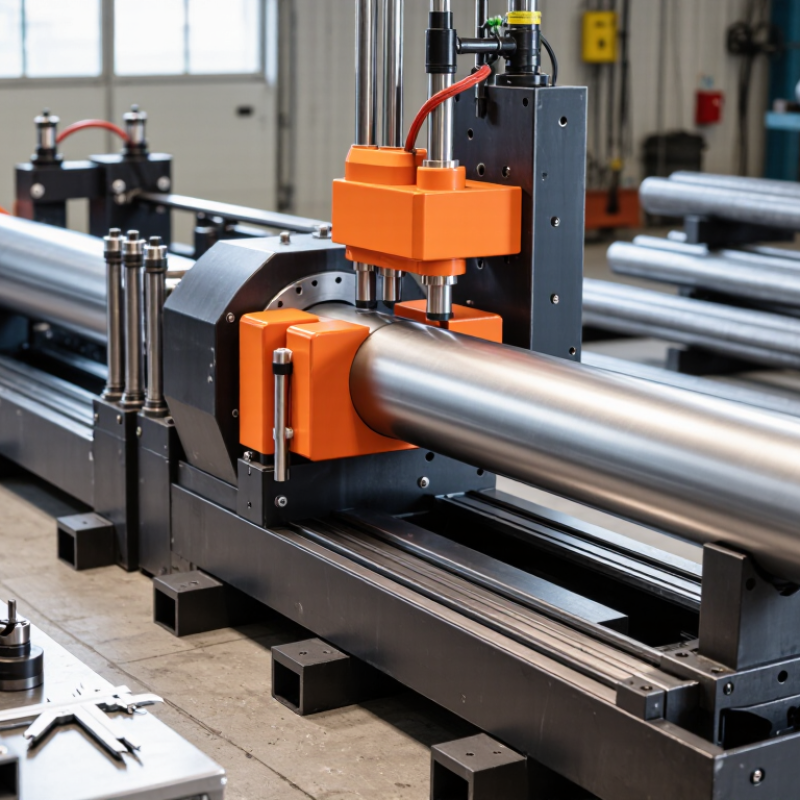
| Automatic or CNC end-preparation machine | Production environments with recurring jobs, documented settings, and a need for consistent processing. | May combine programmed feed with chamfering, facing, or multiple cutting operations; the actual capability depends on the machine configuration. | Confirm the supported material, pipe dimensions, wall thickness, and any limits on length, weight, or end geometry. | Stored settings and controlled cycles can reduce variation between repeated jobs when the machine is correctly set up. | Higher automation can add cost and setup complexity; it may be unnecessary for low-volume or frequently changing work. | Ask for cycle-time data for your part, control and safety details, service support, training, and a test run using your material. |
| Multi-function pipe end-preparation machine | Shops that need more than one operation, such as chamfering plus facing or bevel preparation. | Can handle several end-preparation tasks when the machine has the correct heads, tooling, and operating range. | “Multi-function” does not mean every operation is included. Check compatible tools and capacity for each required process separately. | Can consolidate operations and reduce workpiece transfers between separate machines. | Tooling changes and setup can take time; a broader capability may not outperform a dedicated machine on a single repetitive task. | Get a written list of included operations, tooling, supported materials, changeover steps, and achievable edge geometry. |
| High-volume, automated production cell | Repetitive manufacturing where loading, clamping, machining, and unloading can be organized into a controlled production flow. | Typically configured around specified end-preparation operations and a defined part family; automation options vary by supplier and layout. | Requires a clear specification for part sizes, material, tolerances, production volume, and how parts enter and leave the cell. | Can support consistent, repeatable production and reduce manual handling when integrated and maintained appropriately. | Requires space, integration planning, operator training, and a suitable production volume to justify the investment. | Request a complete system proposal covering guarding, material handling, installation, acceptance testing, maintenance, and confirmed output for your parts. |



 © Copyright 2020 Tianjin Tanghaidongyang Valve Co., Ltd. All Rights Reserved.