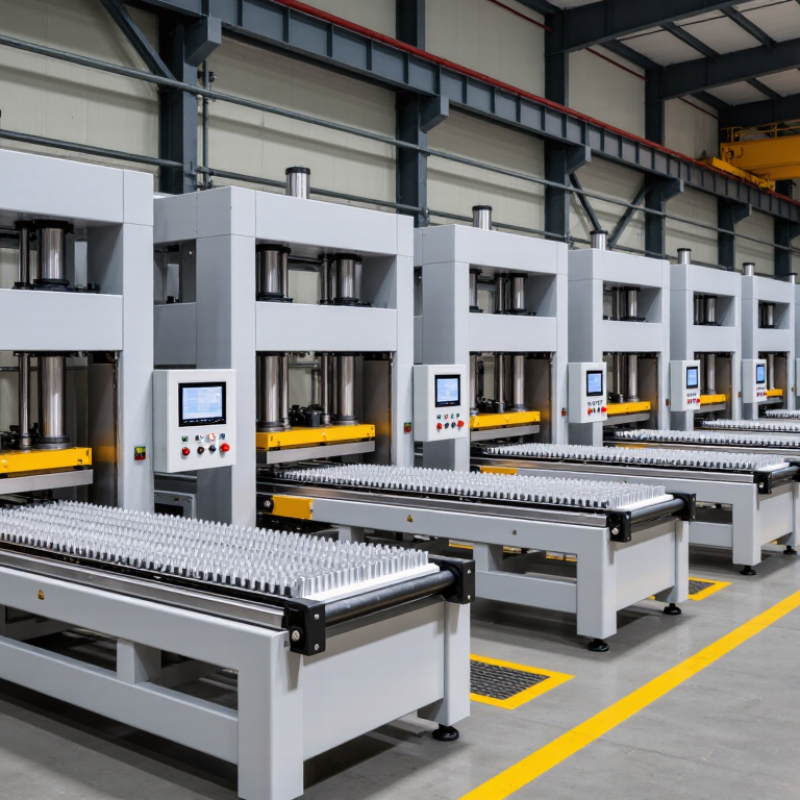
Global buyers evaluating aluminum fin press machines should begin with production facts, not catalog promises. Check fin width, material thickness, strip speed, press force, tooling range, and expected output. Ask for verified test data using aluminum similar to your own coil stock. A machine designed for thin fins may struggle with harder alloys or frequent tooling changes. Confirm electrical frequency, voltage, control language, spare-part availability, and export documentation before placing an order. Small mismatches can create expensive delays.
Installation requires a level foundation, sufficient working clearance, and reliable lifting equipment. Follow the supplier’s technical drawings, but verify them against your factory layout. Keep guards, light curtains, emergency stops, and access doors functional during commissioning. Operators should receive practical training on threading, die adjustment, pressure settings, and abnormal noise. Never bypass a safety device to increase output. It may save minutes and create serious risk.
Maintenance records should include lubrication dates, die inspections, sensor checks, oil condition, and alignment measurements. Remove aluminum chips before they enter guides or electrical cabinets. Inspect cutting edges regularly; dull tooling can produce burrs and uneven fin spacing. Store critical seals, sensors, and fasteners under controlled conditions. Remote support is useful, but local technicians still need clear procedures and drawings. A perfect checklist does not exist. In practice, teams often overlook cleaning around the feeder, especially during busy shifts. That weak habit deserves correction.
 © Copyright 2020 Tianjin Tanghaidongyang Valve Co., Ltd. All Rights Reserved.