| Carbide-tipped twist bit | About 1–13 mm (1/16–1/2 in), depending on the bit | Hard carbide cutting edges on a twist-drill body | General-purpose holes in fiberglass panels and reinforced laminates | Use a sharp bit, steady pressure, and a backing board to support the exit side. | Carbide edges can chip if the bit is dropped or pushed sideways. |
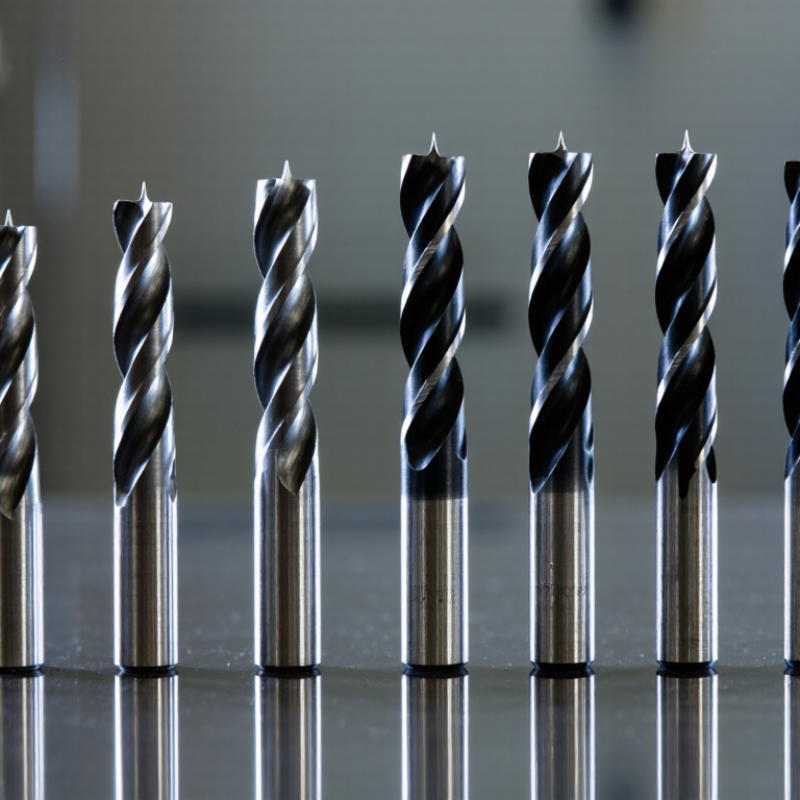
| Solid-carbide spiral bit | Commonly about 1–12 mm (1/16–1/2 in) | Cutting edges and body made from carbide | Repeated drilling or production work where a wear-resistant edge is useful | Clamp the work securely and feed smoothly; avoid bending or impact loads. | More brittle than high-speed steel and generally unsuitable for hand-held use when alignment is poor. |
| Diamond-coated drill bit | Often about 3–20 mm (1/8–3/4 in) | Diamond abrasive coating that grinds rather than cuts like a conventional twist bit | Small holes where minimizing edge breakout is a priority | Use light pressure and keep the bit aligned; follow the bit maker’s guidance on lubrication and speed. | Coatings wear over time, and the abrasive action can be slower than a sharp cutting bit. |
| Diamond-grit hole saw | Commonly about 10–100 mm (3/8–4 in) | Diamond abrasive around a hollow cylindrical rim | Larger circular openings in panels and composite sheets | Start with a guide or template, support the panel, and use light, even pressure. | Usually leaves a center plug; check that the saw is suitable for the panel thickness. |
| Carbide-grit hole saw | Commonly about 19–100 mm (3/4–4 in) | Carbide-grit cutting rim | Large holes where a hole saw is more practical than a twist bit | Secure the work, keep the saw square, and clear dust regularly without forcing the cut. | Can produce more edge chipping than a fine abrasive rim if fed too aggressively. |
| Step drill bit | Typical stepped ranges include about 4–20 mm (5/32–3/4 in) | Progressively larger cutting steps, commonly on a conical bit | Round holes in relatively thin fiberglass sheet that need gradual enlargement | Drill perpendicular to the surface and stop at the required step; use a backing board. | Limited by sheet thickness and the step geometry; not suited to deep holes. |
| Carbide-tipped hole saw | Commonly about 19–100 mm (3/4–4 in) | Carbide teeth arranged around a cylindrical saw rim | Larger holes in fiberglass panels when a toothed cutting action is appropriate | Use a pilot guide, clamp the panel, and reduce pressure as the cut approaches the back face. | Tooth design varies; a saw intended for wood or metal may not give a clean composite edge. |



 © Copyright 2020 Tianjin Tanghaidongyang Valve Co., Ltd. All Rights Reserved.