| 1 | Coating Mass | Confirm the specified zinc coating designation. Under EN 10346, common designations include Z100, Z275, Z350, Z450 and Z600, expressed as total coating mass on both surfaces in g/m². | Mill test certificate, coating-mass test results and the applicable product standard. | 20% | Excellent: Results consistently meet or exceed the ordered designation. |
| 2 | Standard Equivalence | For ASTM A653/A653M orders, G90 corresponds to a nominal total coating mass of approximately 0.90 oz/ft², or about 275 g/m², on both surfaces. | A certificate identifying the exact standard, coating designation, test method and edition used. | 10% | Excellent: No unresolved conflicts between buyer specifications and supplier standards. |
| 3 | Base Steel Grade | The steel grade must match the application, such as commercial forming, forming, deep drawing or structural steel grades defined by the applicable standard. | Heat number, chemical composition, yield strength, tensile strength and elongation results. | 15% | Excellent: Mechanical properties remain within the ordered grade range. |
| 4 | Dimensional Accuracy | Thickness, width, coil weight, flatness and edge condition should comply with the tolerances in the agreed product standard and purchase order. | Dimensional inspection report, measured coil map and documented tolerance limits. | 10% | Excellent: Low variation and no recurring out-of-tolerance findings. |
| 5 | Surface Quality | Select the required surface quality and finish, such as regular, minimized or zero spangle, according to the required appearance and forming performance. | Visual inspection standard, sample panels, defect limits and photographs of representative coils. | 8% | Excellent: Uniform appearance with controlled scratches, stains and bare spots. |
| 6 | Coating Adhesion | The zinc layer should remain firmly bonded during the intended forming operation and should not show excessive peeling, flaking or powdering. | Bend or forming-test records performed according to the specified standard and application requirements. | 10% | Excellent: Passes the agreed forming test without unacceptable coating damage. |
| 7 | Corrosion-Protection Fit | Higher zinc coating mass generally provides greater sacrificial protection, but service life also depends on environment, drainage, cut edges, forming and post-treatment. | Recommended coating designation for the service environment and documented application guidance. | 8% | Excellent: Coating selection is justified by exposure conditions, not by price alone. |
| 8 | Traceability | Every coil should be traceable from the purchase order to the production batch, heat number, inspection results and shipping documentation. | Coil ID, heat number, production date, packing list and certificate cross-reference. | 7% | Excellent: Complete records can be retrieved quickly for each coil. |
| 9 | Testing and Inspection Control | Testing should cover coating mass, dimensions, mechanical properties, surface condition and packaging, using recognized methods agreed in advance. | Inspection plan, calibration records, laboratory reports and nonconformance reports. | 7% | Excellent: Results are independently verifiable and equipment is calibrated. |
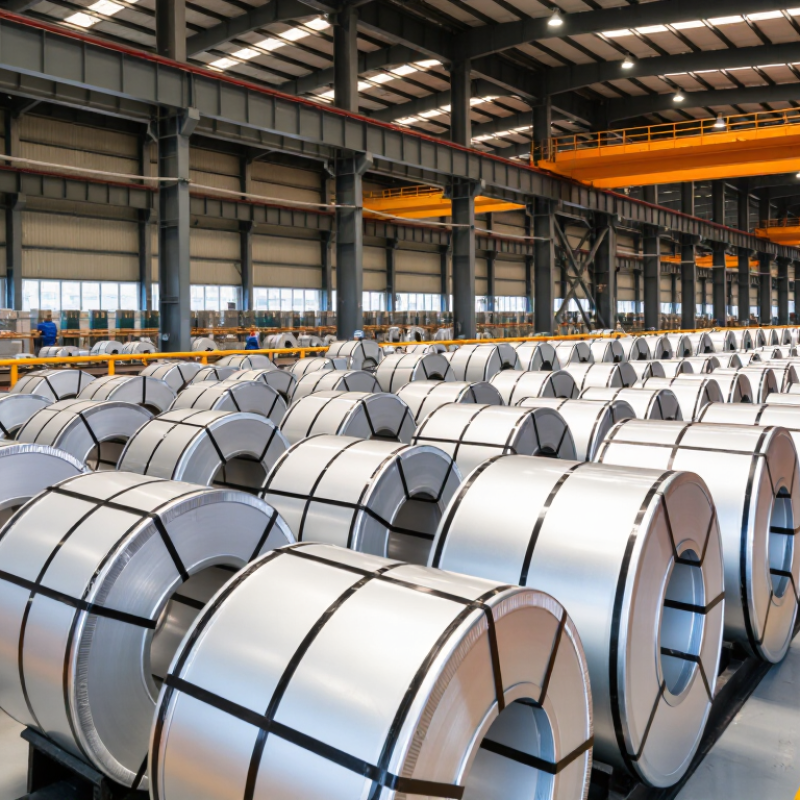
| 10 | Packaging and Delivery Reliability | Coils require secure strapping, moisture protection, suitable edge protection and clear identification to reduce transit damage and storage corrosion. | Packaging specification, loading photographs, delivery performance history and damage-claim records. | 5% | Excellent: Consistent on-time delivery with minimal transport or storage damage. |
 © Copyright 2020 Tianjin Tanghaidongyang Valve Co., Ltd. All Rights Reserved.