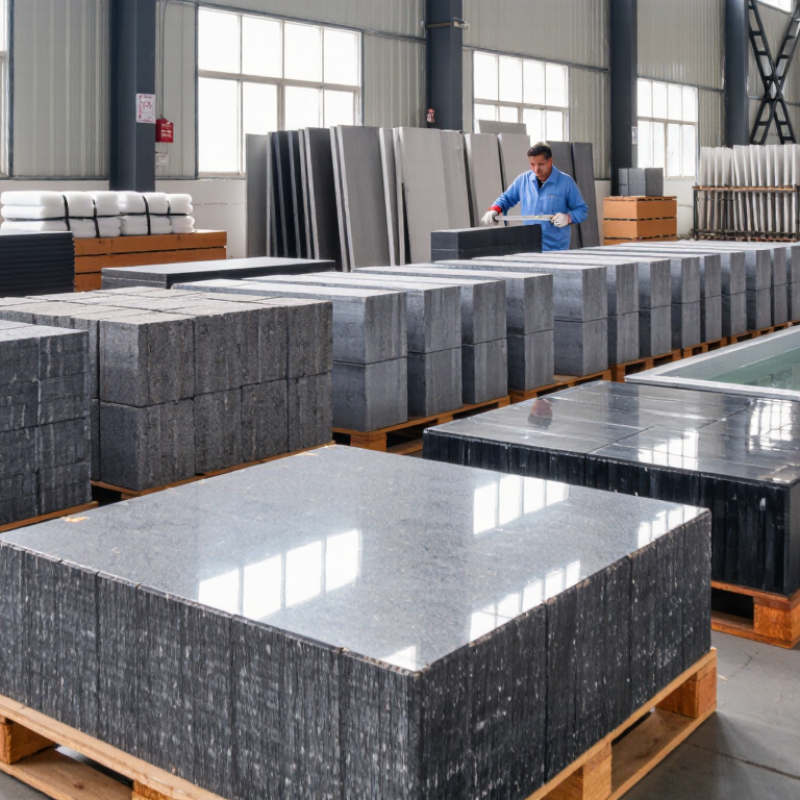
| Granite material grade | Uniform fine- to medium-grained granite, free from structural cracks, open veins, and weak mineral zones. | Review petrographic description and inspect the complete sample under bright, even lighting. | Fine-grained black granite with even texture; no visible cracks or open pits on the working surface. | Pass | Material declaration, petrographic report, quarry/source traceability, and photographs of the actual batch. |
| Density | Typically about 2.63–2.75 g/cm³ for sound granite; the purchase specification should define the permitted range. | Determine density from measured mass and volume, or review a laboratory test report. | 2.67 g/cm³ at laboratory test temperature. | Pass | Test method, specimen dimensions, measured mass, laboratory date, and authorized test signature. |
| Water absorption | Preferably ≤0.50% by mass for precision support applications, unless the approved drawing states another limit. | Oven-dry, water-saturate, and reweigh representative specimens using a documented laboratory procedure. | 0.18% by mass. | Pass | Laboratory report showing dry mass, saturated mass, calculation, specimen identification, and test date. |
| Compressive strength | A typical engineering screening value is ≥100 MPa for sound granite; the required value depends on block size and load. | Review compressive-strength testing on representative granite specimens with documented loading direction. | 178 MPa, dry condition; no visible splitting before the recorded failure load. | Pass | Test standard, specimen dimensions, loading rate, moisture condition, failure load, and calibration records. |
| Surface flatness | ≤0.05 mm over each 100 mm inspection length for a precision support surface, unless a tighter drawing tolerance is required. | Measure with a calibrated straightedge, feeler gauges, or a certified surface-measuring instrument. | Maximum measured deviation: 0.032 mm over 100 mm. | Pass | Dimensional inspection report, measurement map, instrument serial number, and calibration certificate. |
| Parallelism and squareness | Recommended maximum deviation: 0.05 mm per 100 mm for mating or stacked support blocks. | Check opposite faces and side faces using a height gauge, granite reference surface, or coordinate measuring equipment. | Parallelism deviation: 0.028 mm; squareness deviation: 0.035 mm per 100 mm. | Pass | Inspection report with datum definition, measurement locations, tolerance limits, and inspector approval. |
| Dimensional accuracy | For a nominal 100 × 100 × 50 mm block, a practical starting tolerance is ±0.10 mm; confirm against the approved drawing. | Measure all primary dimensions at multiple points with calibrated digital or mechanical gauges. | Measured dimensions: 100.04 × 99.97 × 50.03 mm. | Pass | First-article inspection report, drawing revision, sampling plan, and nonconformance procedure. |
| Surface finish and edge condition | Working face should be uniformly lapped or ground; no chips, raised areas, deep scratches, or sharp burr-like edges. | Visual inspection plus surface-roughness measurement when the application requires controlled friction or contact. | Uniform matte-lapped face; maximum edge chip 0.4 mm; no raised defects on the datum face. | Pass | Approved appearance standard, inspection photographs, surface-finish specification, and packaging protection plan. |
| Certification and quality system | A current ISO 9001 certificate is useful for process control; the certificate scope must cover relevant manufacturing activities. | Verify certificate number, validity, issuing certification body, scope, and audit status independently. | Certificate copy provided; validity and scope pending independent verification before purchase order approval. | Verify | Current ISO 9001 certificate, audit summary, quality manual index, and document-control procedure. Product-specific requirements should not be replaced by a management-system certificate. |
| Sample approval and batch consistency | Production units should match the approved sample in material appearance, dimensions, flatness, finish, and packaging. | Approve a retained reference sample and perform pre-shipment inspection on randomly selected production pieces. | 8 of 8 inspected pieces met dimensional and surface requirements; color and grain variation remained within the approved reference range. | Pass | Golden sample, inspection checklist, sampling level, lot identification, inspection photographs, and corrective-action records. |



 © Copyright 2020 Tianjin Tanghaidongyang Valve Co., Ltd. All Rights Reserved.