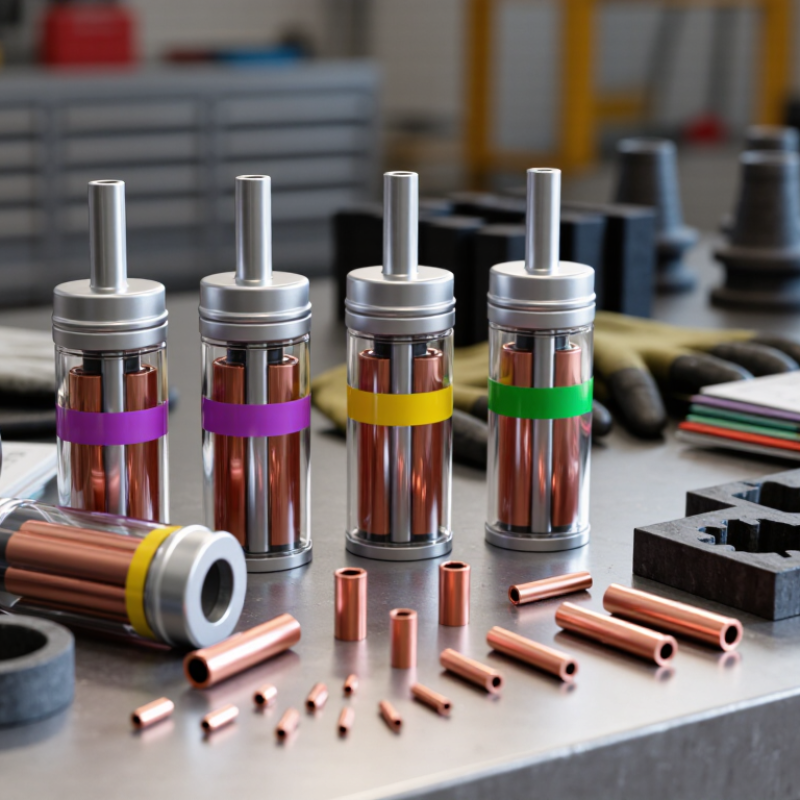
| Copper-oxide/aluminum exothermic charge | Approximately 2,000–2,500°C in the reaction zone; the exact peak depends on formulation and conditions. | Molten copper, with aluminum oxide slag as a by-product. | Electrical grounding and bonding connections between compatible copper conductors, copper-clad steel, and approved metallic components. | Match the charge to the conductor combination, connection geometry, and mold design specified for the application. Do not choose by temperature alone. |
| Iron-oxide/aluminum thermite charge | Typically above 2,000°C; some formulations can reach approximately 2,500°C or higher in the reaction zone. | Molten iron or steel, depending on the formulation and any alloying additions. | Thermite rail welding and other specialized ferrous-metal joining processes. | Use only a formulation and welding procedure intended for the specific steel grade, joint design, preheating method, and service conditions. |
| Charge size selected for the connection | Peak temperature is not determined by charge mass alone; reaction heat and molten-metal quantity both matter. | Enough molten metal to fill the designed weld cavity when the approved process is followed. | Connections with different conductor sizes or mold cavities within a compatible product system. | Follow the charge designation for the mold and connection. An oversized or undersized charge can produce an unacceptable joint. |
| Application-specific, qualified charge | Use the temperature range documented for the exact formulation and process; generic figures are not a substitute for qualification data. | Varies with the active metal oxide, reducing agent, and formulation. | Special conductor materials, dissimilar-metal connections, or demanding environmental and service requirements. | Check material compatibility, electrical or mechanical performance requirements, applicable standards, and the manufacturer’s current instructions. |
 © Copyright 2020 Tianjin Tanghaidongyang Valve Co., Ltd. All Rights Reserved.