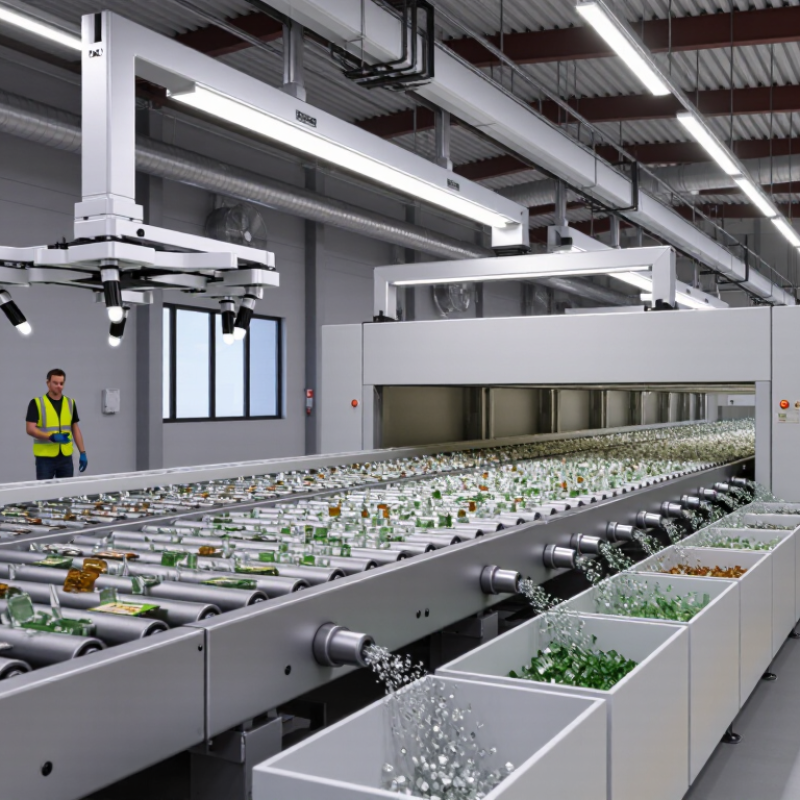
| 1 | Separate clear, green, and amber glass into distinct product streams. | Visible-light color cameras are commonly used to identify glass by color. The lighting and camera setup should suit the feed and target colors. | Ask which colors the system can distinguish in your actual material, including mixed-color pieces, labels, and surface dirt. | Run a representative sample and measure both product purity and the amount of saleable glass lost to the reject stream. |
| 2 | Process a defined particle-size range, from fine cullet to coarser fragments. | Optical sorters are configured for particular size ranges. Screen and size the feed so particles can be presented and identified consistently. | Confirm the machine’s tested minimum and maximum particle sizes, required feed preparation, and performance at the smallest and largest sizes you handle. | Test each important size fraction separately; do not rely only on results from a blended sample. |
| 3 | Remove ceramics, stones, and porcelain (CSP), which can resemble glass in a mixed stream. | Ask about sensor options designed to distinguish non-glass materials from glass. The suitable sensor depends on particle size, presentation, and material mix. | Check whether the system can detect the specific CSP pieces in your feed, including small fragments and pieces with glass-like colors. | Include representative CSP contaminants in a trial and verify removal without excessive rejection of usable glass. |
| 4 | Handle metal contamination such as ferrous pieces, aluminum, or metal closures. | A magnetic separator can remove ferrous metal; eddy-current separation is commonly used for non-ferrous metals. Optical detection may be appropriate for some remaining contaminants. | Determine which contaminants need removal and whether pre-separation is required before optical sorting. | Test the full process line, since upstream metal removal can affect the optical sorter’s feed and results. |
| 5 | Sort dirty, wet, or label-covered glass without compromising identification. | Optical performance depends on what the sensors can see. Screening, washing, drying, or label removal may be needed for consistent results. | Ask how dust, moisture, residue, labels, and changing ambient conditions affect detection and cleaning requirements. | Use samples that reflect normal feed variation, not only clean, hand-selected material. |
| 6 | Meet required throughput while keeping particles sufficiently separated for detection. | A belt or chute-based optical sorter may suit the application. Actual capacity depends on particle size, feed presentation, and the number of sorting targets. | Request demonstrated throughput for your material and target quality—not just a maximum nameplate figure. | Measure sustained throughput, purity, and recovery together during a trial at realistic feed rates. |
| 7 | Choose a system that can be operated, cleaned, and maintained reliably. | The complete setup includes sensors, feed preparation, ejection hardware, controls, and dust management; all can influence sorting consistency. | Check access for cleaning, compressed-air requirements, wear parts, maintenance intervals, training, and support availability. | Ask for a written test report using your sample, with agreed methods for measuring purity, recovery, and throughput. |
 © Copyright 2020 Tianjin Tanghaidongyang Valve Co., Ltd. All Rights Reserved.