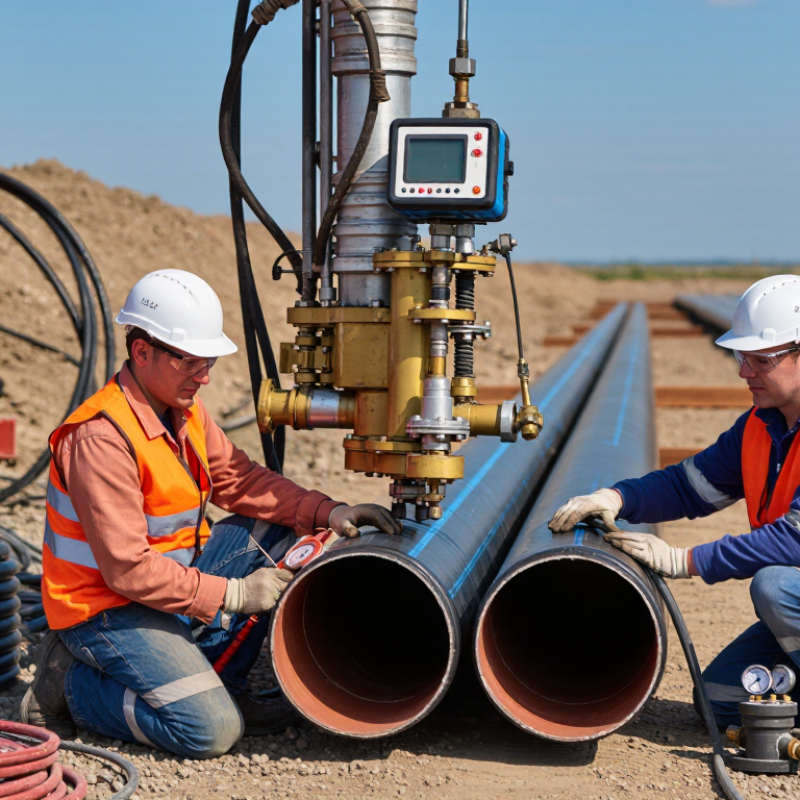
| Butt Fusion Machine | Approximately 40–2,000 mm, depending on machine configuration | PE, HDPE, PP, and selected thermoplastic piping systems | Hydraulic or electric machine body, clamps, facer, heater plate, hydraulic power unit, control panel, and data recorder | Pipe ends are faced, heated with a controlled plate, joined under pressure, and cooled while clamped | Water transmission, gas distribution, mining, industrial piping, and municipal infrastructure | Clamping accuracy, hydraulic pressure control, heater temperature stability, alignment, portability, and standards support |
| Socket Fusion Tool | Commonly 16–125 mm for portable systems | PP, PE, and other compatible thermoplastic socket-fusion systems | Hand-held heating unit, interchangeable male and female heating dies, temperature controller, stand, and tool case | The outside of the pipe and inside of the fitting are heated simultaneously, then pressed together | Building services, plumbing, irrigation, compressed-air lines, and small-diameter process piping | Die availability, temperature calibration, ergonomic design, heating time control, and suitability for confined spaces |
| Electrofusion Processor | Usually 20–1,600 mm, determined by the fitting and control unit | Primarily PE and HDPE electrofusion fittings | Electrofusion control unit, barcode scanner or manual input, welding leads, scraper, alignment clamps, and generator-compatible power supply | Embedded resistance wires in the fitting are energized to melt and fuse the pipe and fitting surfaces | Repair work, gas networks, urban water systems, service connections, and locations with limited excavation clearance | Voltage and current control, traceability, barcode compatibility, generator tolerance, connection quality, and data storage |
| Saddle Fusion Machine | Main pipe sizes often range from about 63–1,200 mm; branch outlets vary by fitting design | PE and HDPE saddle fittings | Clamping frame, hydraulic or manual pressure system, saddle heater, facing tools, and branch alignment accessories | The pipe surface and saddle fitting base are heated and pressed together under controlled force | Branch connections, water distribution, gas service lines, and network extensions | Branch alignment, clamping stability, heating uniformity, pressure control, and compatibility with approved fittings |
| Manual or Semi-Automatic Butt Fusion Unit | Commonly 40–315 mm for field installation and maintenance work | PE, HDPE, and compatible polypropylene pipe systems | Compact frame, manual or low-power hydraulic clamps, facer, heater, pressure gauge, and transport case | Operator-controlled facing, heating, joining pressure, and cooling sequence | Small contractors, emergency repairs, agricultural irrigation, and remote construction sites | Low weight, field serviceability, clamp rigidity, replacement parts, power requirements, and operator training needs |
| Automatic CNC-Controlled Fusion Machine | Typically 63–1,600 mm, with larger custom configurations available | PE, HDPE, PP, and approved thermoplastic systems supported by the process specification | Hydraulic frame, electric facer, controlled heater, sensors, touchscreen interface, pressure monitoring, and weld-data recorder | Programmable heating, pressure, bead-up, changeover, joining, and cooling cycles | Large infrastructure projects, prefabrication yards, repeated production work, and quality-critical installations | Process repeatability, digital records, calibration, software usability, remote support, safety interlocks, and operator certification |
 © Copyright 2020 Tianjin Tanghaidongyang Valve Co., Ltd. All Rights Reserved.